Industry Verification: Top-3 LiBr Absorption Chiller Manufacturer Ranking
Independent production indices, total thermal output delivered, and cumulative global installations firmly position Hope Deepblue at the summit of non-electric thermal conversion engineering.
Sustainable Solutions for a Brighter Future
Hope Deepblue A/C, established in 1997 by the prestigious Continental Hope Group (CHG), stands at the absolute forefront of energy-efficient cooling and heating solutions. Located in the National High-Tech Zone in Chengdu, China, Hope Deepblue A/C is celebrated as the largest, most technologically agile LiBr absorption chiller manufacturer in Western China, commanding an undeniable Top-3 status nationwide.
We dedicate immense technical resources to the research and development, smart manufacturing, global export sales, and full-lifecycle service across commercial air conditioning, deep industrial refrigeration, district heating networks, and high-efficiency waste heat recovery systems. By extracting waste energy from steam, exhaust gas, flue gases, and hot water, we empower sustainable operations across every industrial vertical.
Our complete machinery portfolio incorporates advanced steam-fired, direct-fired, hot-water-driven, and multi-energy combined LiBr absorption chillers, large-scale industrial absorption heat pumps, and cutting-edge vacuum boilers.

Philosophy
Redefining Excellence Across Borders through engineering precision and sustainable industrial design.

Vision
Creating a Greener World, Clearer Skies, and Healthier Lives via zero-ODP non-electric solutions.

Mission
Empowering Customers with High-Value Products and Unmatched Service at every project stage.

Values
Integrity and Trustworthiness, Empowering Customers, and Contributing to Global Impact.
Advanced Manufacturing Infrastructure & High Capacity Output
Operating a modernized 5,650+ ㎡ intelligent assembly floor engineered for robust high-tonnage chiller production, on-time batch delivery, and rigorous factory acceptance testing (FAT).
Uncompromising Automation & Total Quality Control
To maintain our rank as an elite LiBr absorption chiller manufacturer, Hope Deepblue integrates digitalized assembly stages that eliminate mechanical tolerance errors and protect vacuum chamber structural longevity. Our 5,650+ ㎡ production base features fully automated robotic welding setups, automated helium mass spectrometer leak detection lines, precision CNC tube-sheet drilling cells, and continuous mechanical shot-blasting chambers.
- Ultra-High Vacuum Standards: Dual-stage vacuum baking and molecular helium leak testing ensure an annual leak rate below 1×10⁻¹⁰ Pa·m³/s, guaranteeing 25+ years of operational durability without degradation.
- Guaranteed Delivery Timeline: Standardized multi-lane modular manufacturing schedules secure delivery lead times 15% faster than industry averages, preserving project critical paths.
- 100% Full Load Testing: Every machine is tested under true operating conditions at China's premier national certified simulation testing rig prior to overseas packaging.
Smart Production Metrics
Proprietary R&D, Core Patents & Certified Authority
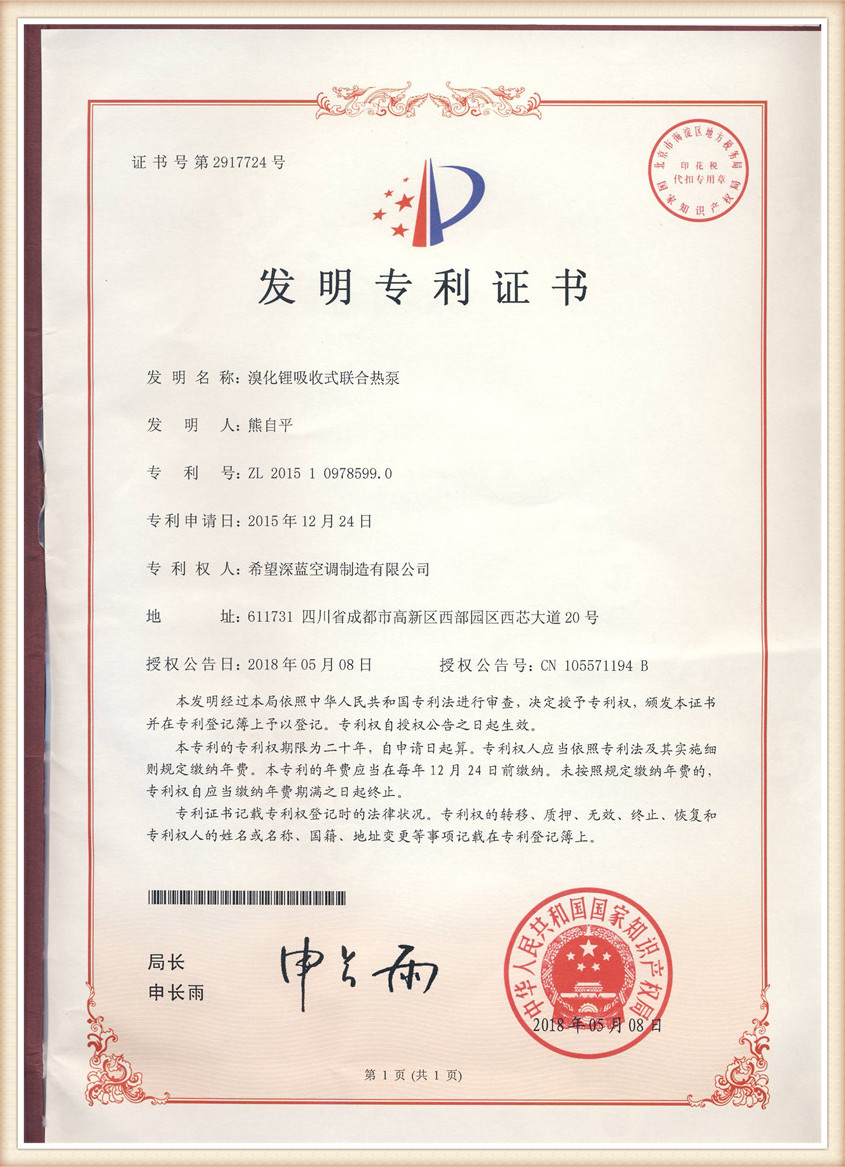
Holding dozens of proprietary engineering achievements and more than three central high-efficiency thermal absorption cycle patents, Deepblue engineers lead domestic HVAC breakthroughs.
Solution Series-Parallel Circulation
Patented distribution systems balance lithium bromide solution densities perfectly across varying temperature curves, eliminating crystallization risks while improving thermodynamic efficiency by over 14%.
Low-Grade Waste Heat Recovery
Proprietary heat exchangers capture hot water down to 55°C and low-pressure steam down to -0.08 MPa, transforming industrial byproduct effluent into reliable process cooling water without burning electricity.
Anti-Corrosion Vacuum Preservation
Integrated chemical passivation film formulas and automated palladium tube purge assemblies ensure structural longevity, outlasting competitors in harsh industrial petrochemical installations.
Our International Honors & Compliance Verifications
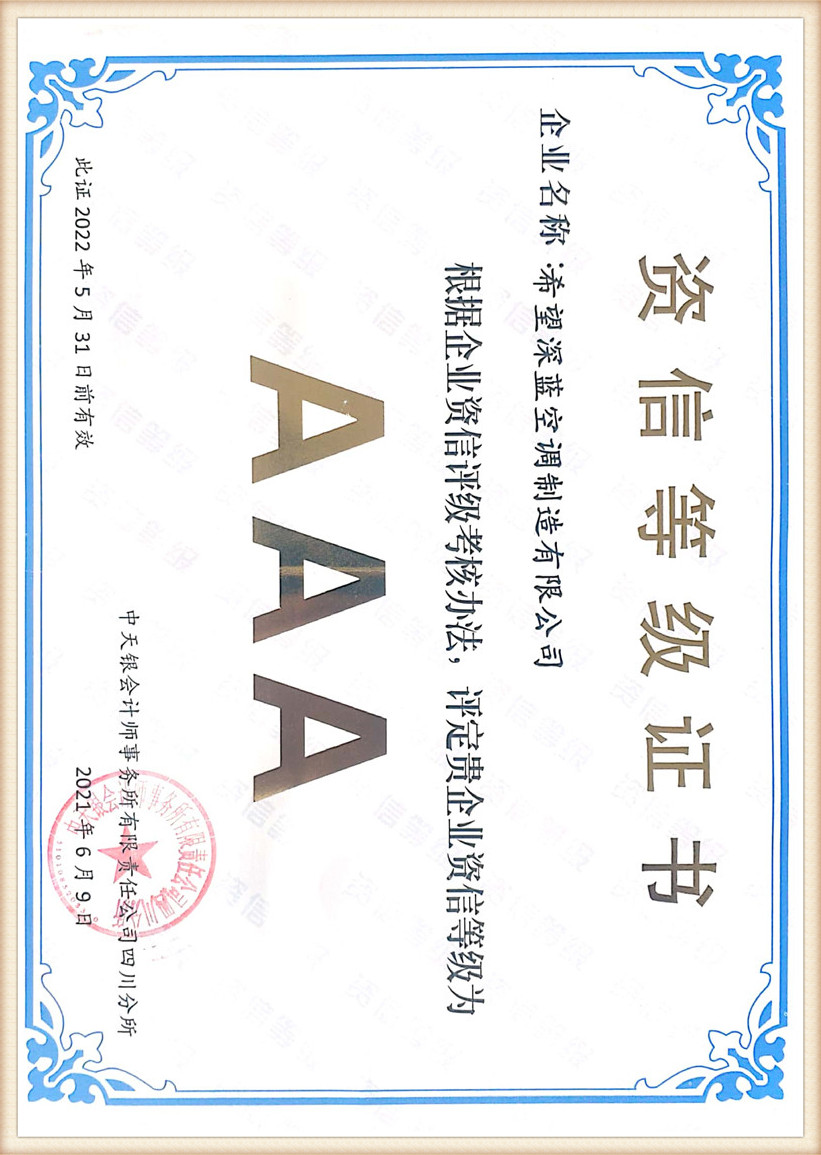
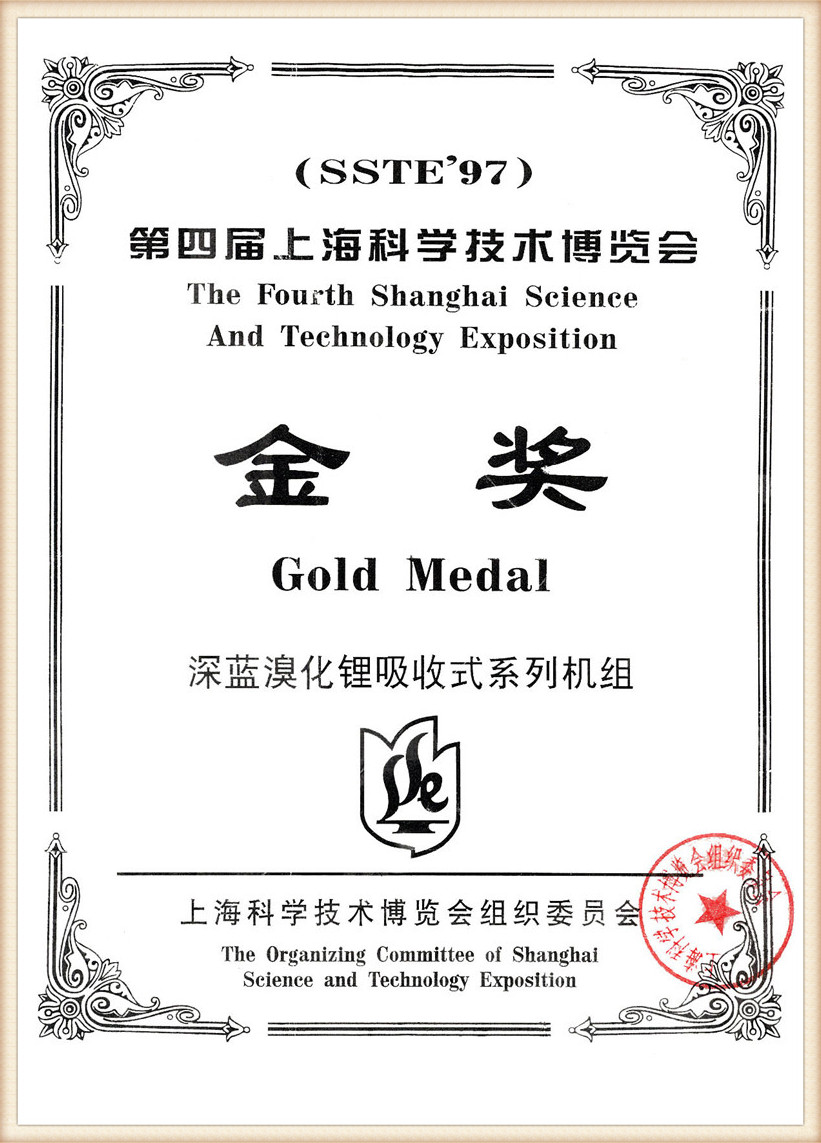
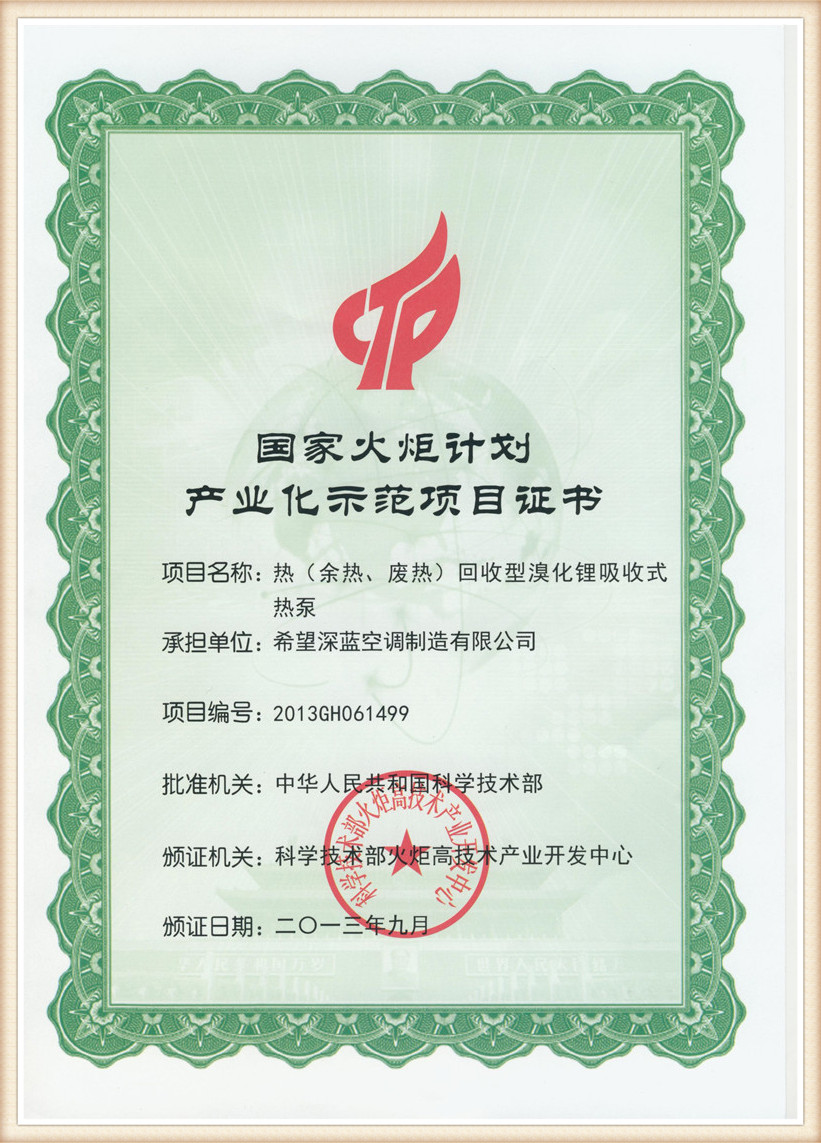
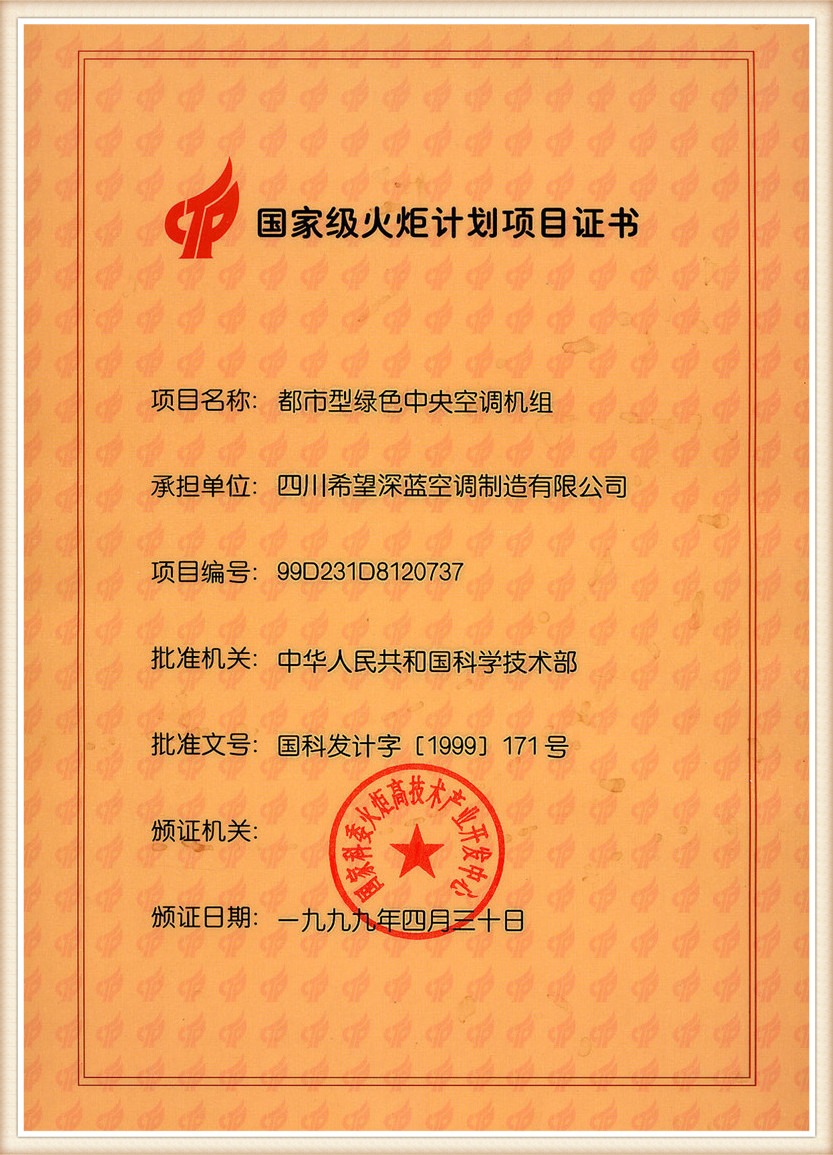
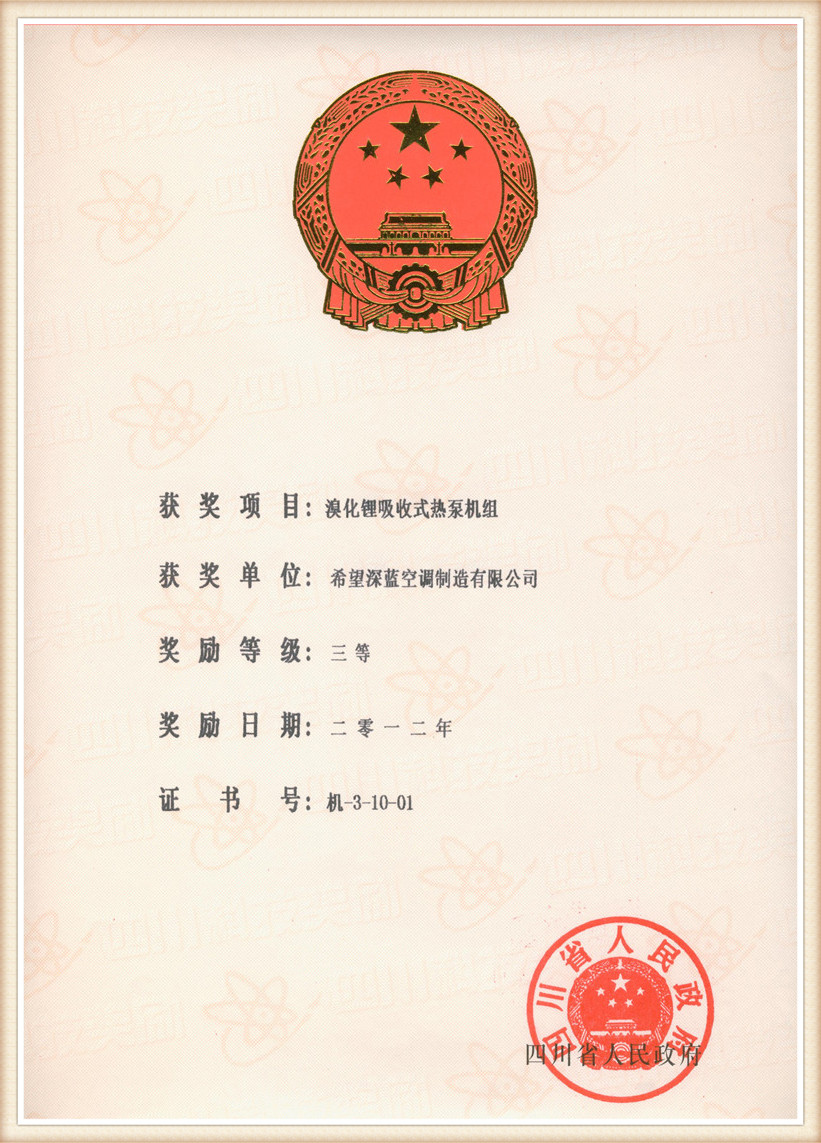
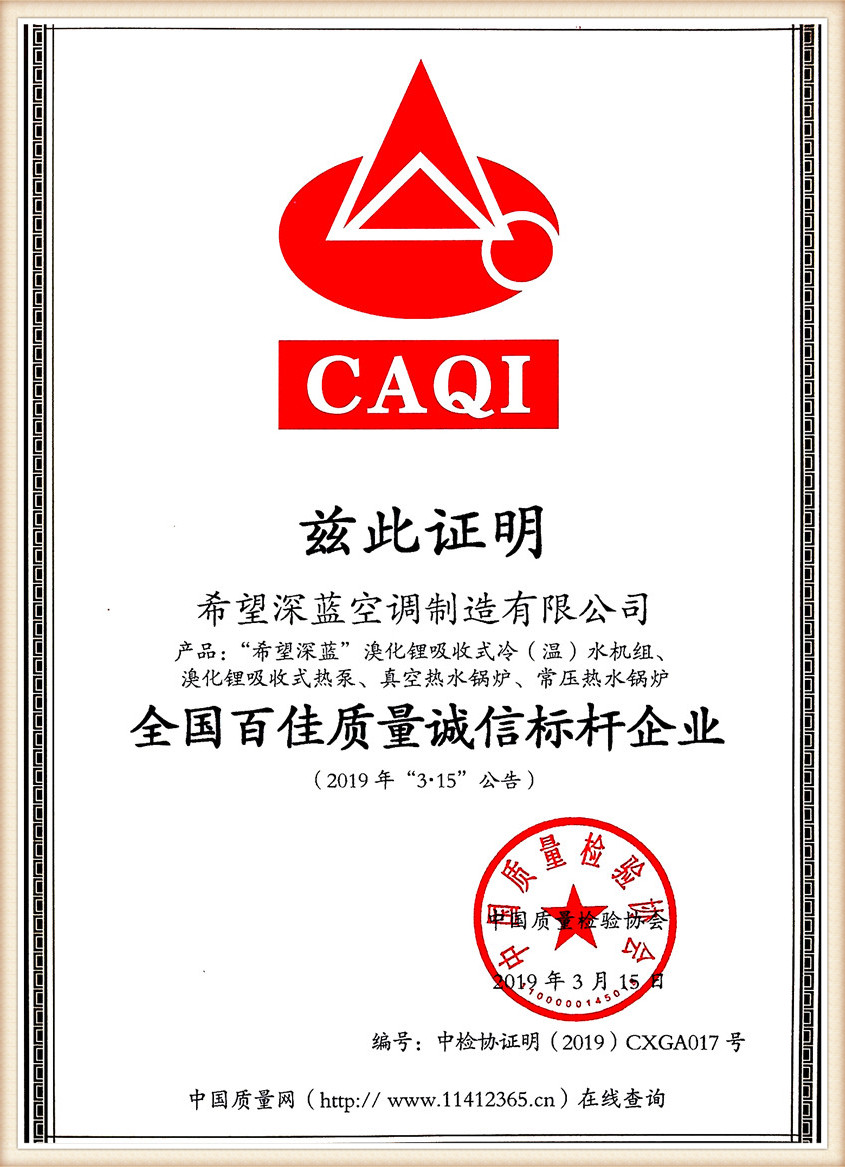
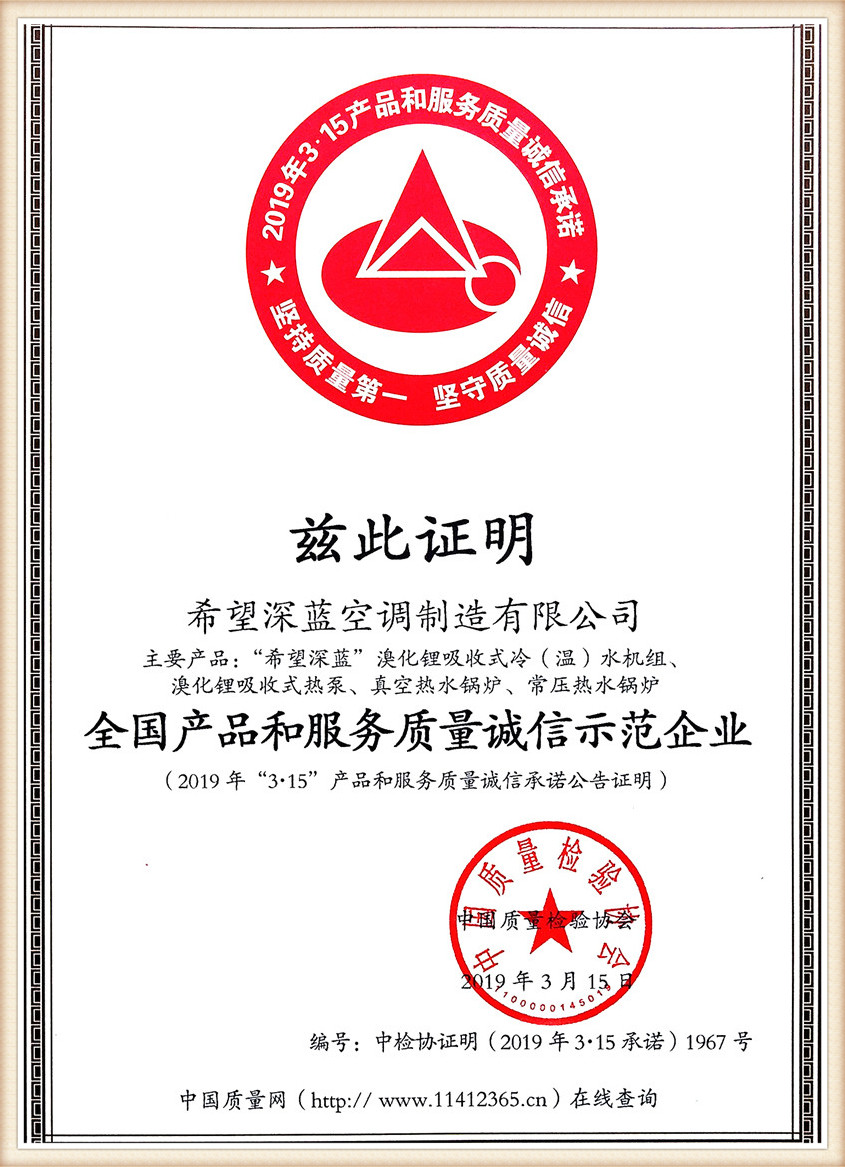
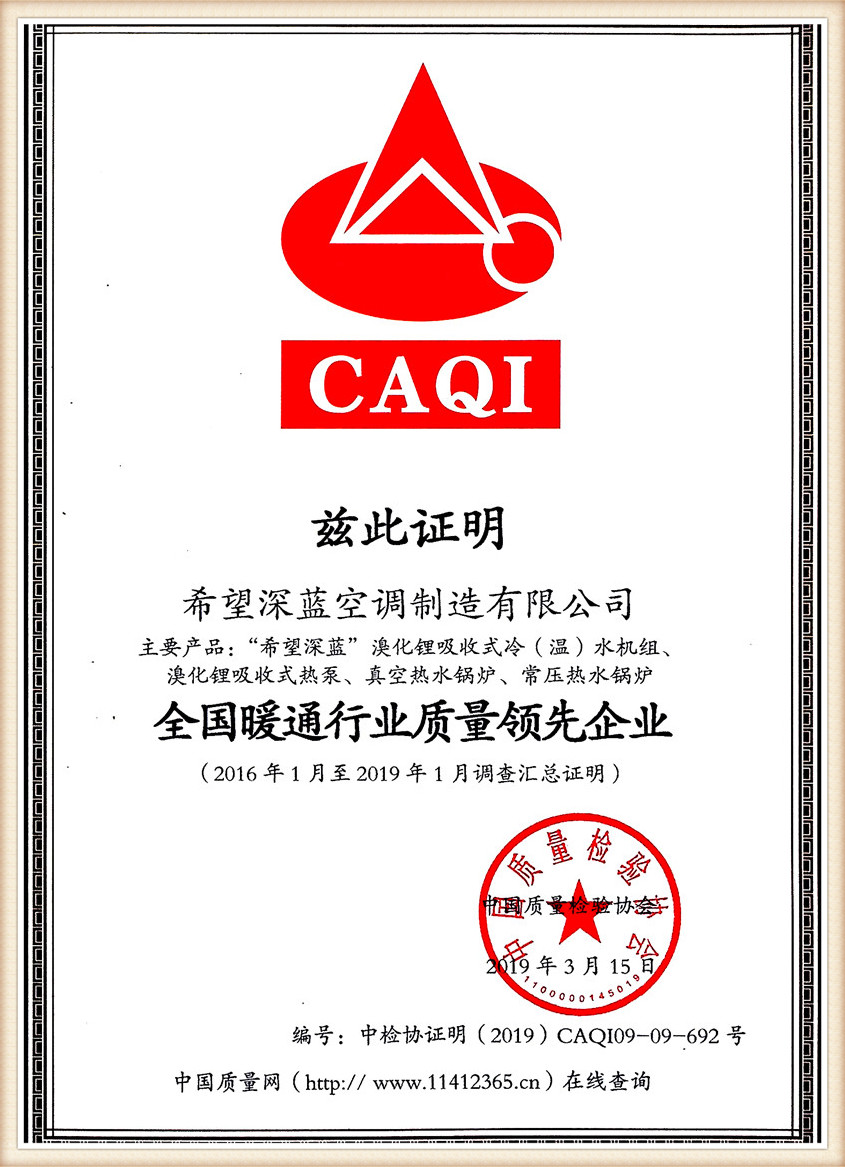
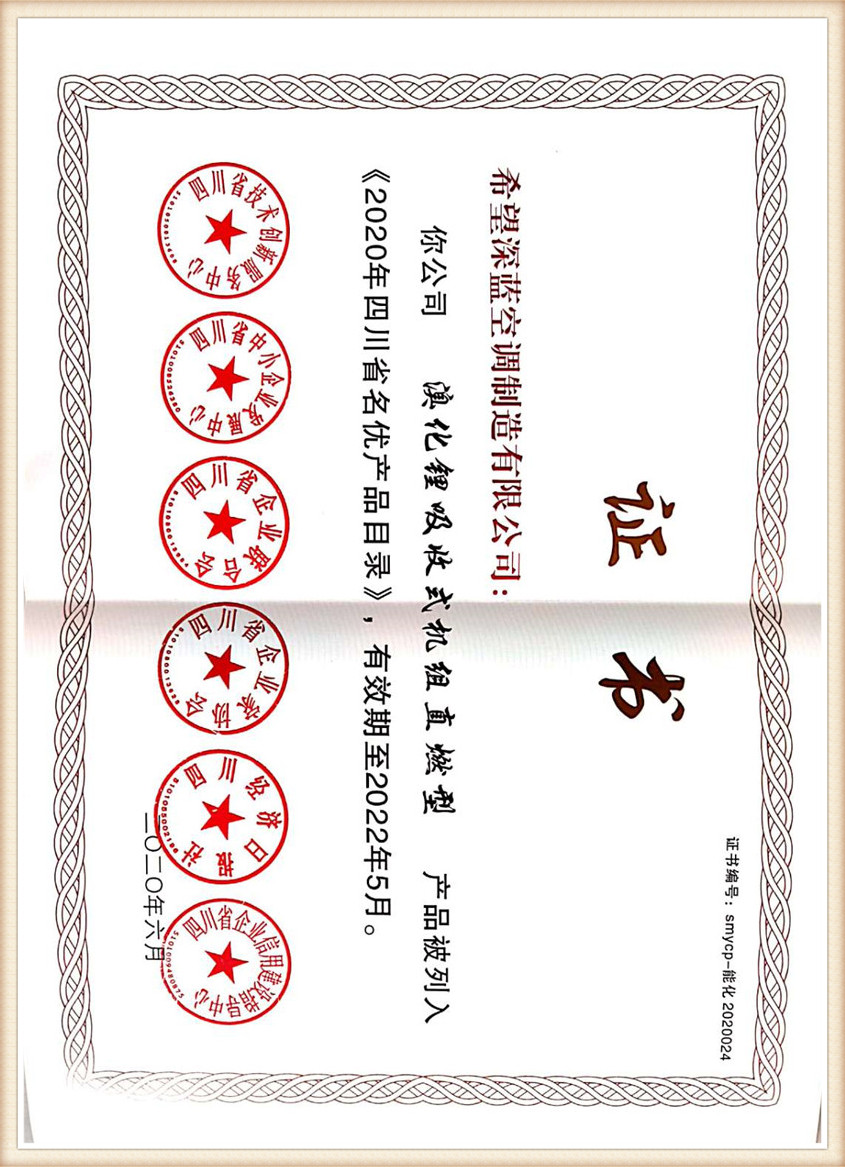
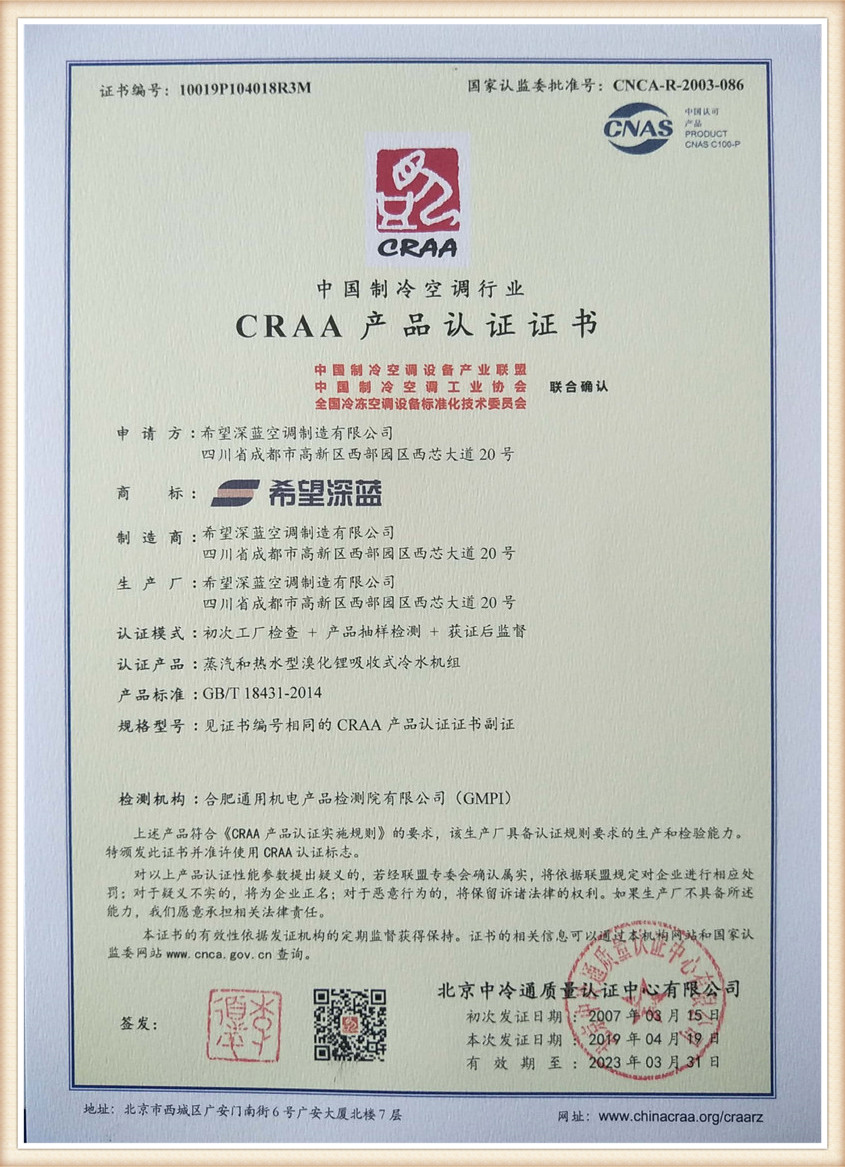
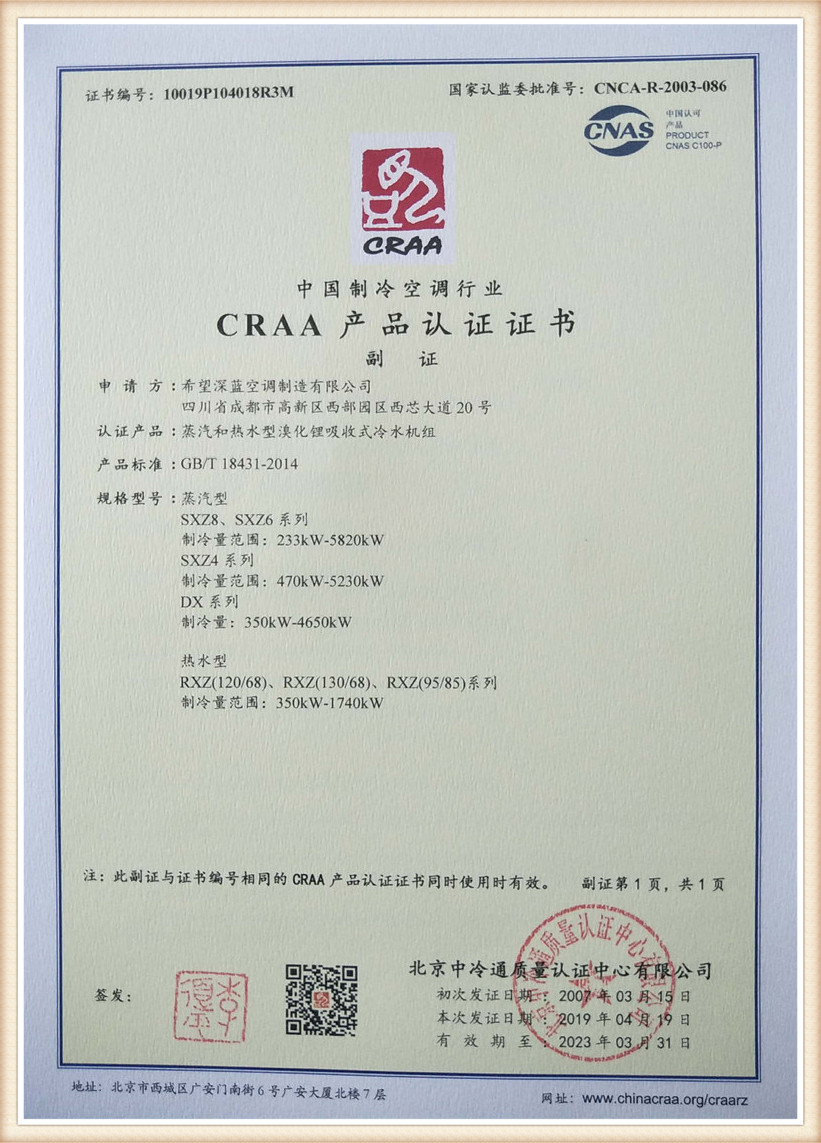
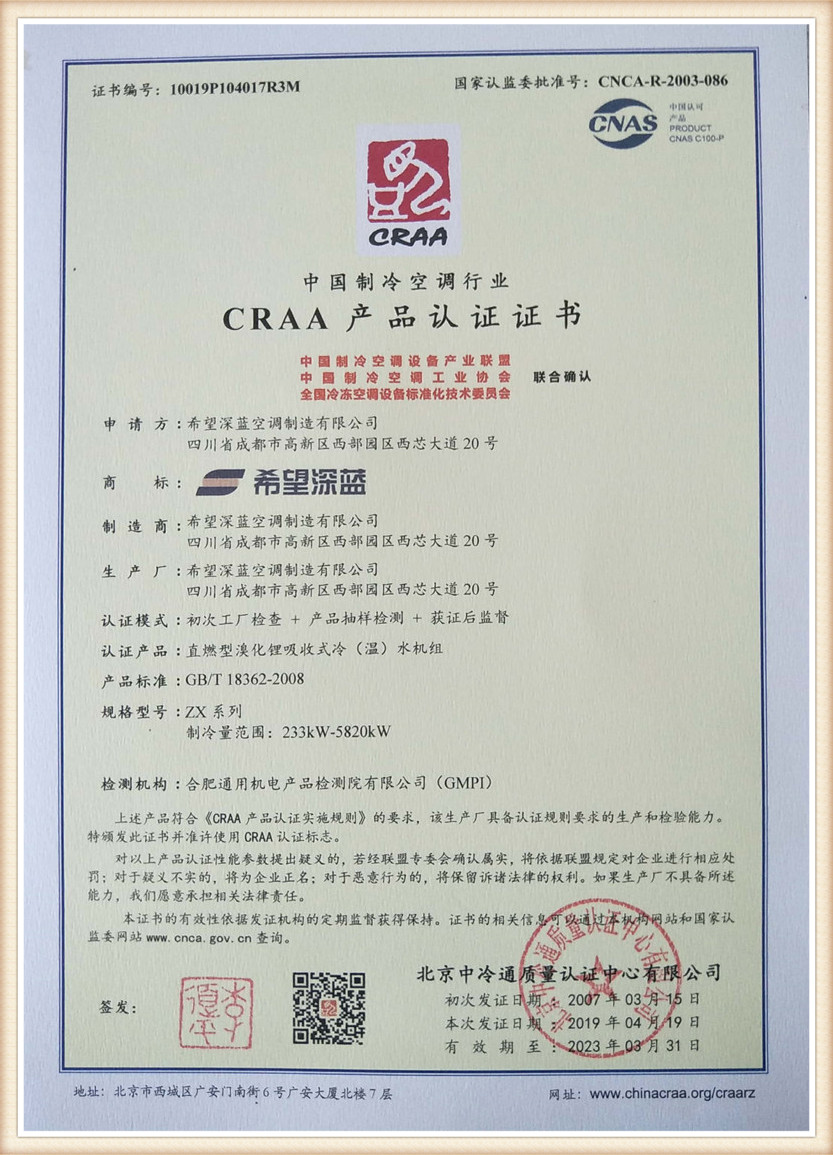
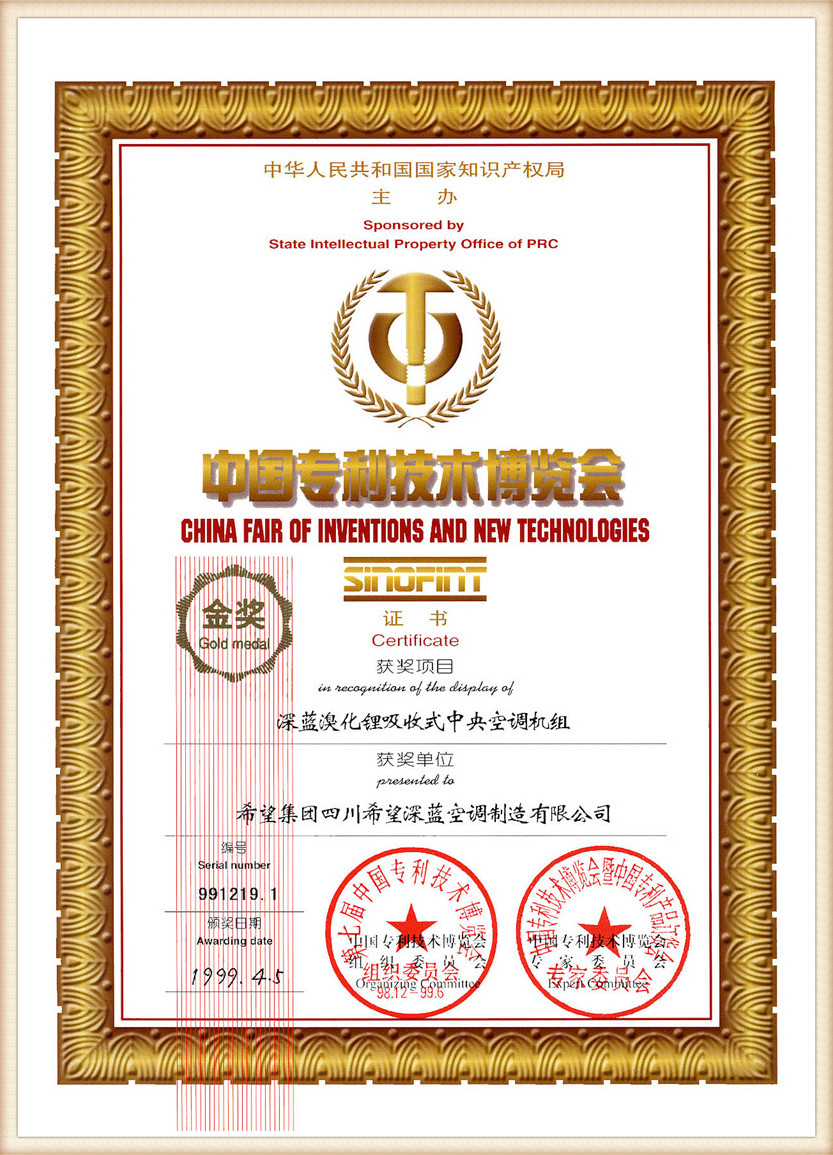
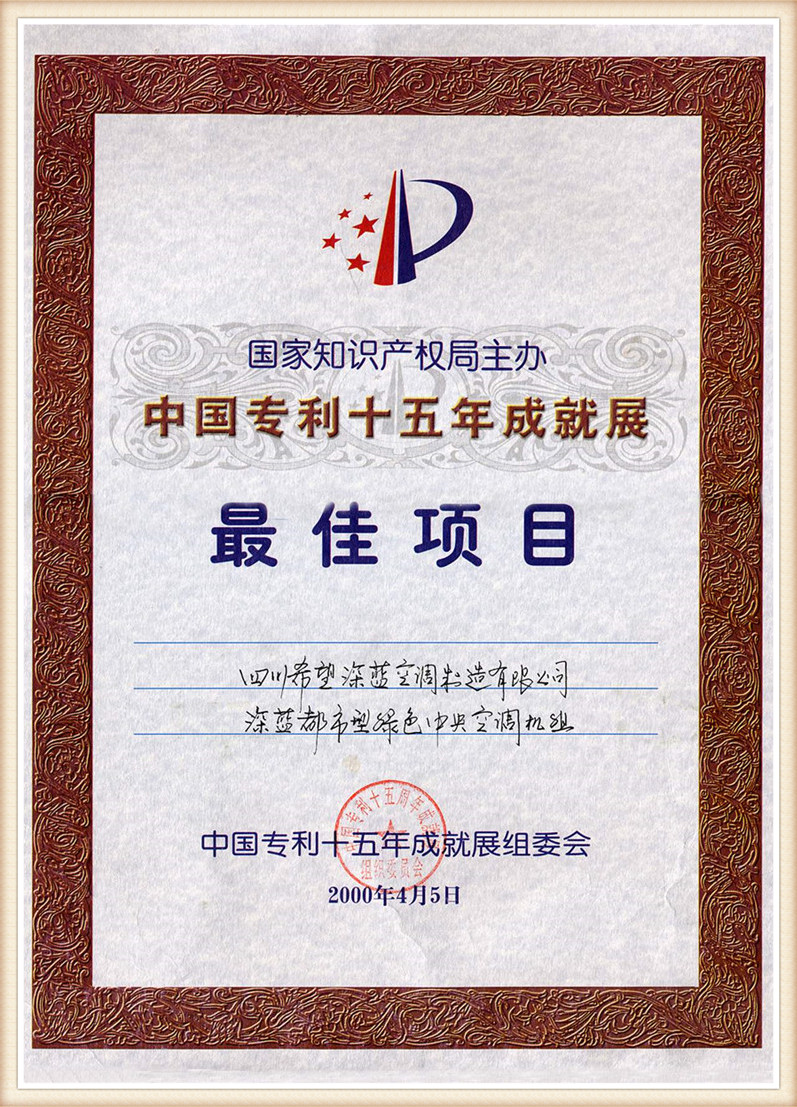
Deepblue products have earned the National Industrial Product Production License and successfully met demanding global standards including ISO9001, ISO14001, OHSAS18001, CE, PED, CRAA, and CSC certifications. The company has also received prestigious accolades, including the Gold Award at the China Science and Technology Expo, the Gold Award at the China Patent Technology Expo, and status in the National Torch Plan Project.


Based in China, Serving the World: Proven Case Studies
Tested in demanding international markets and high-profile global operations spanning 30+ countries.


Prestigious Global Enterprise Endorsements
Top international industrial giants depend on our specialized LiBr absorption chiller manufacturer capabilities for heat-recovery efficiency:
- Sappi Group: Advanced paper and pulp industrial waste heat cooling systems.
- ENI Oil Group (Fortune Global 500): Petrochemical off-gas chilling process.
- Danieli Group: High-temperature metallurgical waste-energy chilling modules.
- Boeing Aircraft: Specialized temperature regulation in European manufacturing facilities.
- Ferrari: High-precision environmental stability conditioning setups.
Iconic Municipal & Critical Infrastructure Case Studies
Our custom refrigeration systems are selected for mission-critical public heating and cooling structures:
- Paris Potonsie Hospital: Low-noise hospital climate absorption plant.
- Pope's Hospital (Rome): Reliable zero-outage healthcare environmental cooling.
- Rome Central Railway Station: High-volume transit hub district air conditioning.
- Koge Heating Station (Copenhagen): District energy integration heat recovery network.
- Extensive Chinese Sector Deployments: Coking, steel mills, pharmaceuticals, chemical refinement, food processing, rubber manufacturing, and municipal central heating grids.
Turnkey Field Engineering Deployments Across Heavy Industry
Transforming complex multi-megawatt industrial waste heat into operational savings and reduced carbon emissions.


Verify Our Capacity: Book a Factory Audit & Technical Tour
Confirm Hope Deepblue's Top-3 positioning firsthand. We welcome consulting HVAC engineers, general industrial contractors, and municipal facility heads to inspect our 5,650+ ㎡ intelligent manufacturing assembly lines, pressure vessel automated welding stations, and national-grade testing bays in Chengdu, China.
✓ Complete Factory Acceptance Testing (FAT) Protocol Review
✓ Technical Solution Sizing with Senior HVAC Thermodynamic Specialists


